See how leading businesses solve real operational challenges with our industrial solutions.
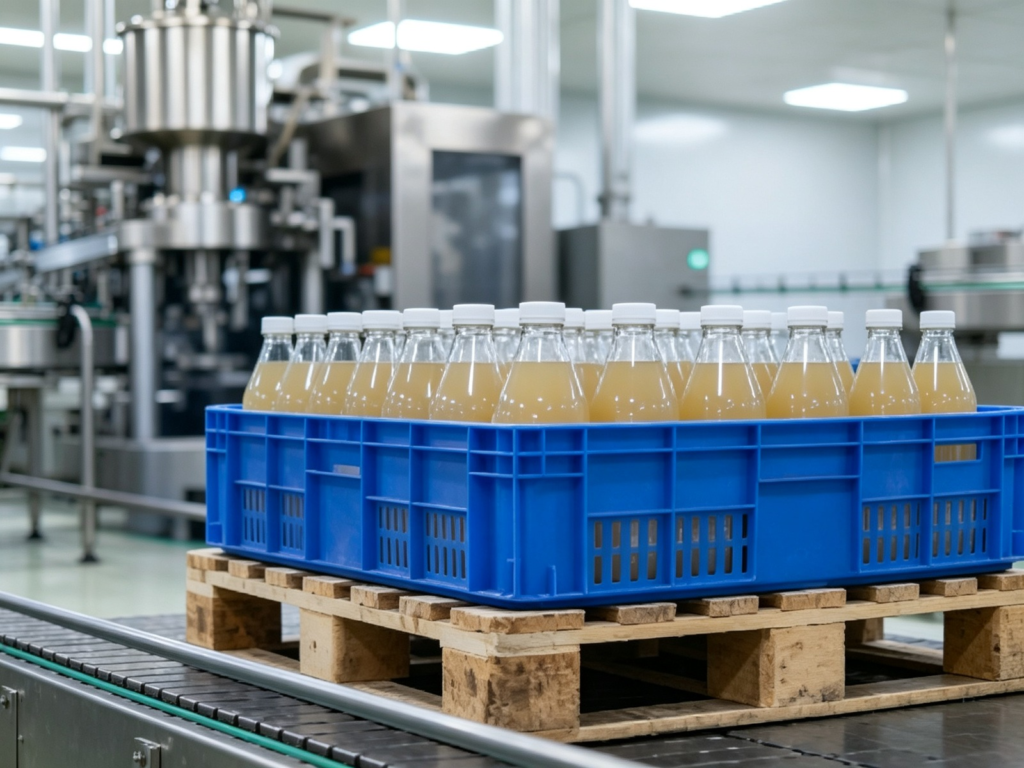
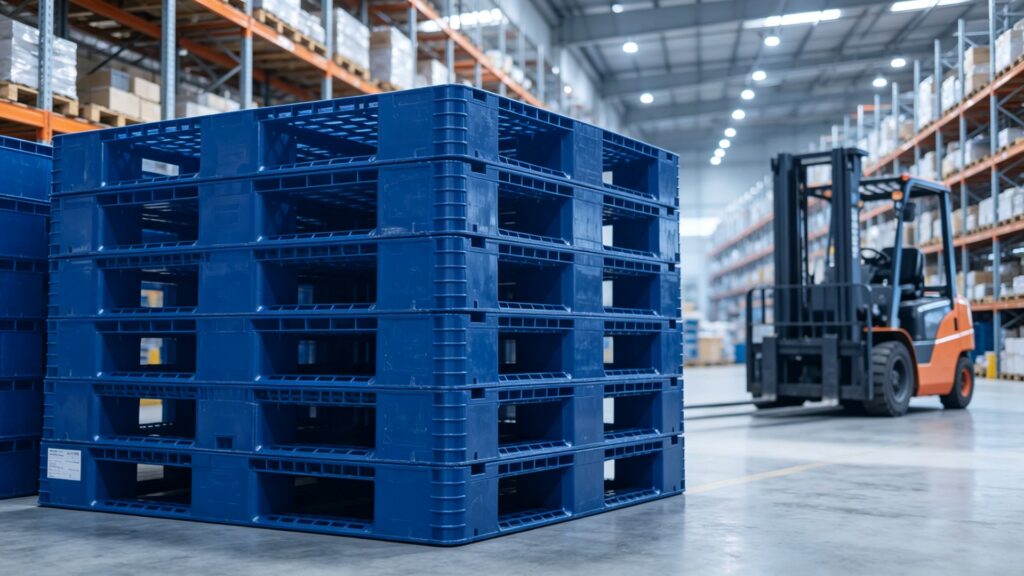
From high-bay racking to cross-docking, logistics and warehousing operations depend on material handling equipment that keeps goods moving safely and efficiently. Our plastic pallets are engineered to handle the rigors of 24/7 distribution environments, reducing downtime, lowering replacement costs, and improving warehouse safety.
Food-grade hygienic pallets helped Naturale Foods pass FDA audits with zero non-conformances and reduced product contamination incidents by 100%.
Food safety is paramount in the FMCG industry. Naturale Foods was experiencing 2–3 contamination incidents per year traced back to wooden pallet debris. Their internal audit team flagged the pallet program as a high-risk area, and they faced potential production shutdown risks during FDA inspections.
CHT-P1210-HG, CHT-P1111-LD — Our hygienic pallet line, specifically the CHT-HG1210 and CHT-HG1111 models, was selected after rigorous testing. These one-piece injection-molded pallets feature a smooth, non-porous surface that can be pressure-washed and sanitized. Made from FDA-approved virgin HDPE, they are completely safe for direct food contact. Our team conducted on-site trials at 3 facilities and validated the pallets against their HACCP requirements.
pressure-wash friendly design
3 years for wood
“Food safety is non-negotiable for us. Switching to Chenhui Tong’s hygienic pallets eliminated a major source of contamination risk. Our last three FDA audits had zero findings related to pallets — that’s unprecedented in our industry.”
— Dr. James Chen, VP of Quality Assurance, Naturale Foods Group
Tell us about your requirements and our engineering team will deliver a custom quote
with product recommendations within 24 hours.
We typically reply within a few hours